Olaprixa Industrial
Discover our core high-performance water treatment and filtration systems designed for strict industrial and municipal compliance.
A globally trusted manufacturer and specialized engineering provider redefining pollutant removal technology standards.
Shanghai Olaprixa Industrial Co., Ltd. is a specialized manufacturer and engineering provider focused on advanced industrial wastewater treatment solutions, integrating sludge processing systems and intelligent chemical dosing technologies. Headquartered in Shanghai, China, the company delivers efficient, reliable, and customized water treatment systems for a wide range of industries including manufacturing, chemical processing, food production, and municipal infrastructure.
Olaprixa offers a comprehensive portfolio covering wastewater treatment equipment, sludge dewatering and thickening systems, and precision chemical dosing units designed to optimize treatment performance and operational efficiency. By combining modern process engineering with automation control, the company ensures stable system operation, reduced environmental impact, and compliance with global discharge standards.
With a strong emphasis on customization, Olaprixa provides tailored water engineering solutions based on specific project requirements, from initial consultation and system design to installation guidance and after-sales technical support. Its team of experienced engineers continuously works to enhance system efficiency, reduce energy consumption, and improve resource recovery. Committed to sustainability and innovation, Shanghai Olaprixa Industrial Co., Ltd. aims to help global clients achieve cleaner production, water reuse, and long-term environmental responsibility through smart and cost-effective treatment technologies.
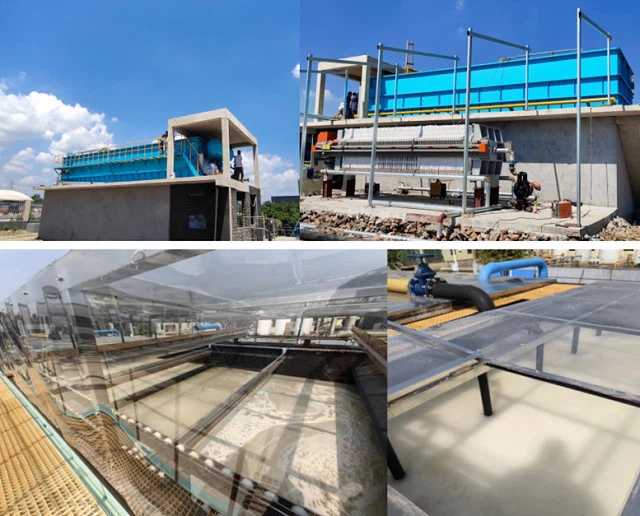
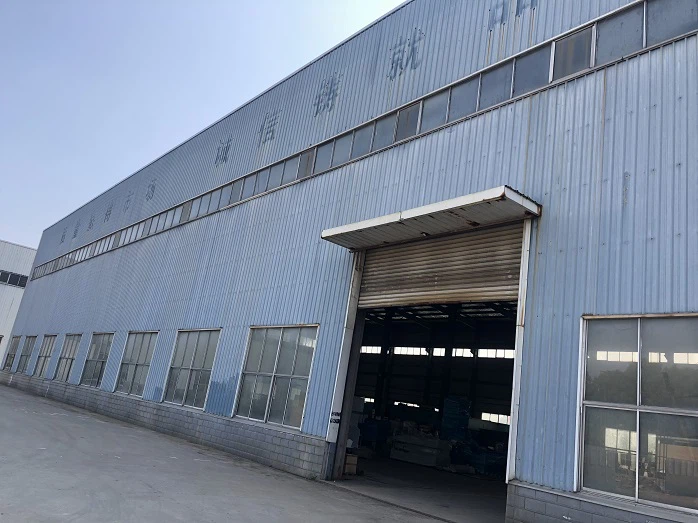
Backed by rigorous R&D, advanced fabrication lines, and thousands of successful global deployments.
Analyzing why international engineering contractors and municipal authorities source pollutant removal technology from premier Chinese manufacturers.
China's industrial clusters provide robust supply chain integration for raw materials, precision pumps, corrosion-resistant piping, and PLC automation modules. This lowers production lead times and reduces capital expenditure without compromising structural integrity.
Top-tier suppliers implement strict quality control protocols—ranging from ultrasonic weld testing and hydrostatic pressure checks to electrical insulation audits—ensuring equipment longevity in aggressive chemical and wastewater environments.
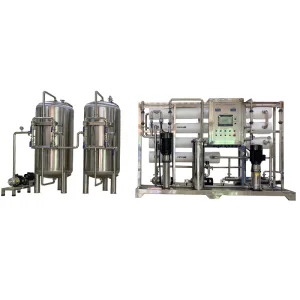
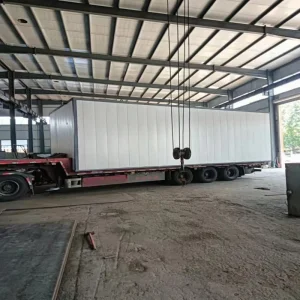
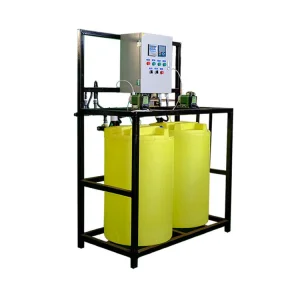
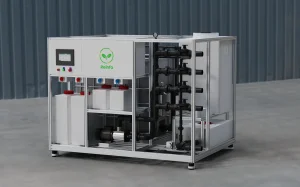
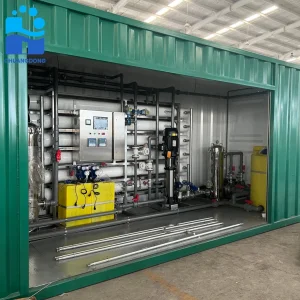
Modern plant operators demand plug-and-play mobility. Containerized reverse osmosis plants and skid-mounted dosing units minimize site installation time, reducing civil engineering costs dramatically for remote or fast-track projects.
Navigating international environmental standards and future-proofing industrial wastewater infrastructure.
Meeting regional discharge limits (such as EU Water Framework Directives, US EPA standards, and local BOD/COD thresholds) requires adaptable process configurations. Our systems feature multi-barrier treatments combining biological A/O processes, MBR, and advanced membrane filtration to guarantee compliance under fluctuating influent conditions.
The industry is rapidly shifting toward smart water grids powered by IoT sensors, automated dosing algorithms (PAM/PAC optimization), and Zero Liquid Discharge (ZLD) systems. These innovations minimize waste disposal volumes, recover valuable salts/water, and drastically lower facility carbon footprints.
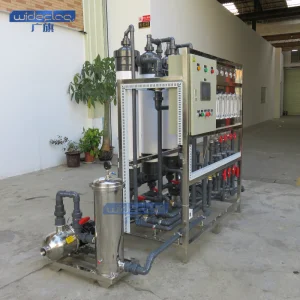
Explore our extended line of specialized sludge dewatering, containerized RO systems, and agricultural dosing solutions.
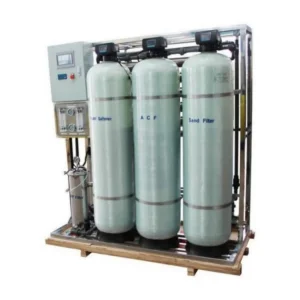
Integrated Water Clarification Filtration and Disinfection System for Surface Water Treatment Plants
View Details
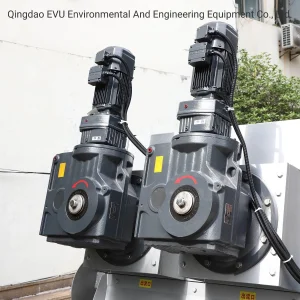
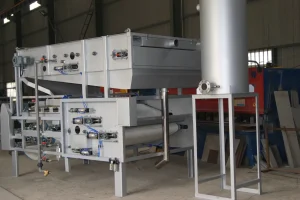
Sewage Treatment System and Domestic Waste Water Treatments Plants Sludge Dewatering Equipments
View DetailsExpert answers regarding custom engineering, equipment installation, and global export support.
We conduct a thorough water quality analysis based on your specific COD, BOD, heavy metals, or salinity parameters. Our engineering team then designs a modular combination of biological processes (A/O, MBR), membrane filtration (RO/UF), and precision chemical dosing tailored to your exact discharge standards.
Containerized RO or wastewater treatment plants are pre-assembled, pre-tested, and housed within standard ISO shipping containers. This ensures rapid on-site deployment, minimal civil work requirements, weather protection, and easy relocation if project sites change.
Yes. All our core electrical panels, dosing systems, and filtration units are built in accordance with CE, ISO9001, and international electrical/safety standards, ensuring smooth customs clearance and regulatory acceptance worldwide.
We provide comprehensive remote technical guidance, detailed 3D installation manuals, PLC programming support, and video troubleshooting. On-site commissioning and engineer dispatch services are also available upon request for large-scale projects.