Olaprixa Industrial
Next-generation real-time analytical monitoring, automated chemical metering, and IoT-enabled fluid feedback systems tailored for demanding industrial environments.
Modern industrial processing demands dynamic accuracy, operational safety, and resource optimization. As industrial standards in the Grenville regional economy escalate, process engineers can no longer rely on traditional static chemical dosing pumps or manual calibration methods. Modern operations require adaptive, autonomous closed-loop intelligent dosing control systems designed to adjust reagent inputs dynamically based on real-time fluid diagnostics.
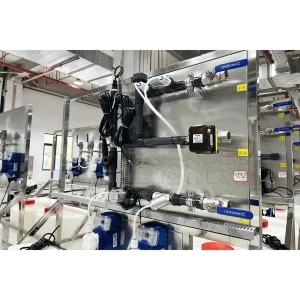
An Intelligent Dosing Control System integrates high-precision metering pumps, multi-parameter electrochemical sensors (pH, ORP, conductivity, turbidity, residual chlorine), variable frequency drives (VFDs), and programmable logic controllers (PLC) running proprietary self-learning control algorithms. By continuously analyzing changing process streams, these systems eliminate chemical under-dosing (which risks regulatory non-compliance and batch degradation) and over-dosing (which incurs inflated operational expenditures and damages downstream membrane assets).
For enterprises seeking qualified Intelligent Dosing Control System suppliers for the Grenville market, key procurement vectors extend beyond pure hardware specifications. Engineering decision-makers must evaluate local environmental compliance frameworks, system interoperability with legacy SCADA architecture, modular scalable skid design, and total life-cycle maintenance costs. This comprehensive industry whitepaper breaks down technical methodologies, localized implementation engineering, global supply chain synergies, and procurement strategies to help Grenville facilities achieve zero-defect operational control.
Analyzing local municipal mandates, industrial water reclamation standards, and industrial process automation needs within Grenville.
Industrial facilities operating across Grenville face increasingly stringent environmental regulations governing municipal effluent discharge, total dissolved solids (TDS), trace heavy metal precipitation, and chemical oxygen demand (COD). Uncontrolled chemical injection during effluent neutralization leads to compliance penalties and environmental liabilities. Intelligent chemical dosing controllers deployed in Grenville utilize real-time proportional-integral-derivative (PID) feedback algorithms to maintain strict pH and coagulation chemistry windows, ensuring full compliance with local discharge threshold mandates.
From commercial food and beverage processing lines requiring precise CIP (Clean-In-Place) sanitation cycles to rubber compound blending and battery manufacturing, Grenville's commercial base demands automated reliability. Manual dosing of biocides, anti-scalants, or slurry additives introduces human error and production downtime. Intelligent dosing systems delivered to Grenville feature standardized Modbus TCP/IP, Ethernet/IP, and 4-20mA telemetry interfaces, bridging seamlessly into local facility control systems.
Our intelligent dosing system architecture for Grenville is engineered for harsh environment durability, supporting local power grid variations, weather-resistant NEMA 4X / IP66 enclosures, remote remote-access diagnostic modules, and modular component replacement to guarantee near-zero operational downtime.
To understand the technological superiority of our intelligent chemical dosing platforms, we must analyze the closed-loop control architecture that underpins high-precision fluid dynamics.
Multi-sensor arrays continuously record system flux, feed flow rate, temperature, fluid electrical conductivity, ORP, and specific ionic concentrations. Analytical signals are filtered via digital noise reduction before entering the primary processor.
Unlike standard static timer dosing systems, our PLC logic evaluates dynamic change rates. If flow volume suddenly spikes or water chemistry shifts, the algorithm adjusts pump stroke length and pulse frequency dynamically.
Solenoid-driven or motor-driven diaphragm pumps respond to variable stroke commands within milliseconds, providing micro-dosing accuracy across low flow rates up to industrial high-volume discharge capacities.
| Subsystem Component | Technical Specification Range | Operational Benefit for Grenville Facilities |
|---|---|---|
| Main Logic Controller | Siemens S7-1200 / Allen-Bradley Micro800 Series | High reliability, global spares availability, native SCADA integration. |
| Metering Pump Drive | Digital Stepper Drive / Frequency-Inverter Motor | Turn-down ratios up to 1000:1, pulse-free continuous chemical dispersion. |
| Fluid Contact Materials | PVDF, PTFE, SS316L, Hastelloy C-276, Ceramic Valves | Maximum chemical resistance against aggressive acids, alkalis, and solvents. |
| Communication Protocols | Modbus RTU/TCP, Profinet, 4-20mA HART, Cloud IoT | Real-time remote cloud telemetry and mobile alert capabilities. |
Global Supply Chain Capabilities, Rigorous Quality Control, and Direct Factory Engineering Advantage for Grenville Enterprise Buyers.
Shanghai Olaprixa Industrial Co., Ltd. is a specialized manufacturer and engineering provider focused on advanced industrial wastewater treatment solutions, integrating sludge processing systems and intelligent chemical dosing technologies. Headquartered in Shanghai, China, the company delivers efficient, reliable, and customized water treatment systems for a wide range of industries including manufacturing, chemical processing, food production, and municipal infrastructure.
By combining modern process engineering with automation control, Olaprixa ensures stable system operation, reduced environmental impact, and compliance with strict global discharge standards. The integration of advanced OEM/ODM manufacturing processes allows Olaprixa to deliver premium intelligent dosing systems to Grenville clients at highly competitive direct-factory pricing.
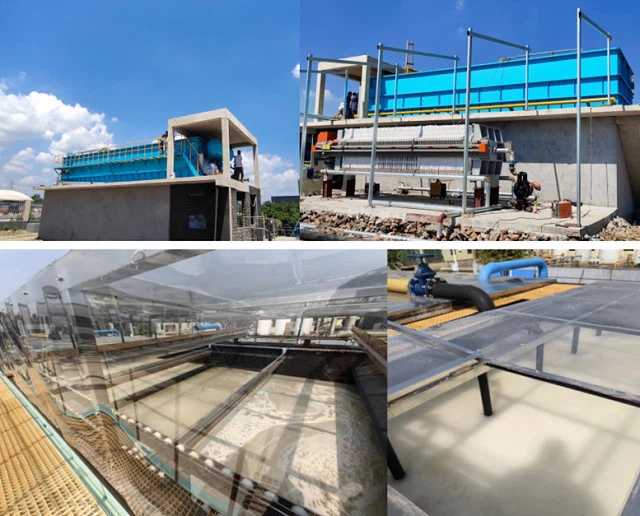
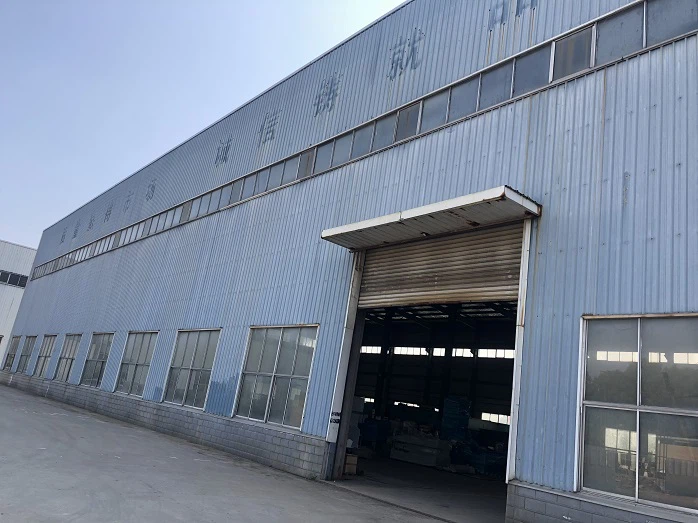
Olaprixa offers a comprehensive portfolio covering wastewater treatment equipment, sludge dewatering and thickening systems, and precision chemical dosing units designed to optimize treatment performance and operational efficiency.
With a strong emphasis on customization, Olaprixa provides tailored water engineering solutions based on specific project requirements, from initial consultation and system design to installation guidance and after-sales technical support. Its team of experienced engineers continuously works to enhance system efficiency, reduce energy consumption, and improve resource recovery.
Committed to sustainability and innovation, Shanghai Olaprixa Industrial Co., Ltd. aims to help global clients achive cleaner production, water reuse, and long-term environmental responsibility through smart and cost-effective treatment technologies.
Discover how specialized intelligent dosing control systems address distinct sector challenges in Grenville.
Precision dosing of coagulants, flocculants, sodium hypochlorite, and bisulfite for municipal raw water clarification and effluent compliance in industrial parks. Closed-loop residual feedback maintains water safety without chemical waste.
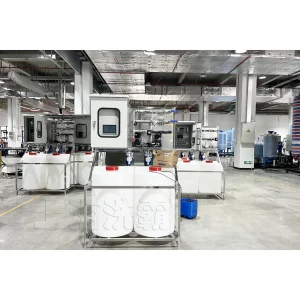
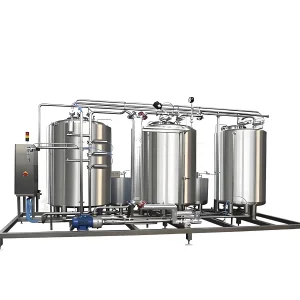
Automated concentration-based chemical dosing (caustic soda and acid wash solutions) for clean-in-place processing lines. Smart electrical conductivity feedback ensures stringent food safety standards while reducing wash cycle times.
Ultra-precise high-viscosity pumping systems engineered to handle abrasive, high-solid lithium slurries and chemical reagents without clogging, maintaining uniform flow rate accuracy for high-tech manufacturing plants.
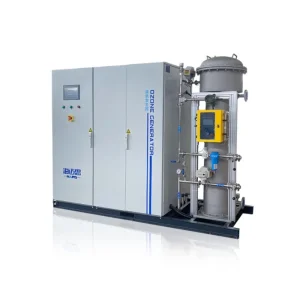
Integrated high-output ozone generation control skids (3,000g/h to 10,000g/h) with dynamic dissolved ozone concentration feedback for advanced oxidation processes (AOP), biological disinfection, and color removal.
Protects expensive RO membranes from silica and calcium carbonate scaling by precisely pacing antiscalant injection proportional to raw water feed flow rates and conductivity metrics.
PLC-controlled automated dry chemical powder weighing and liquid polymer batching systems engineered to maximize batch consistency and physical properties in rubber compound production.
Explore our full line of field-tested dosing skids, flow controllers, CIP chemical systems, and high-precision fluid units available for immediate global export.
Purchasing automated chemical dosing control systems involves evaluating total cost of ownership (TCO), engineering compliance, and localized post-sales support. Procurement teams in Grenville should utilize the following 4-step framework to evaluate prospective equipment suppliers:
Verify whether the system uses true continuous PID closed-loop feedback or basic timed pulse dosing. Ensure the control cabinet supports multi-parameter sensors (e.g., pH, conductivity, ORP, flow rate) native to your plant's operational chemistry.
Specify exact concentration and temperature profiles of chemical reagents (e.g., concentrated H2SO4, NaOH, FeCl3, PAM). The supplier must provide certified PVDF, PTFE, or 316L/Hastelloy wetted components to prevent premature seal failure.
Demand rigorous FAT documentation including hydrostatic pressure testing, electrical safety checks, signal integration simulation, and ISO 9001 compliance prior to export shipping to Grenville project sites.
Partner with direct OEMs like Shanghai Olaprixa who offer comprehensive spare parts kits (diaphragms, check valves, sensor probes) and provide fast global logistics to eliminate production interruptions.
Technical insights and purchasing guidance for plant managers and system integrators in the Grenville market.
Consult with our senior fluid automation engineers to design a customized, energy-efficient intelligent chemical dosing control skid tailored to your specific application requirements.
Send Inquiry Now