 Olaprixa Industrial
Driven by strict environmental regulations and global net-zero targets, industrial manufacturing demands high-performance, sustainable water purification ecosystems. Shanghai Olaprixa Industrial Co., Ltd. stands at the forefront of this industrial transition.
Shanghai Olaprixa Industrial Co., Ltd. is a specialized manufacturer and engineering provider focused on advanced industrial wastewater treatment solutions, integrating sludge processing systems and intelligent chemical dosing technologies. Headquartered in Shanghai, China, the company delivers efficient, reliable, and customized water treatment systems for a wide range of industries including manufacturing, chemical processing, food production, and municipal infrastructure.
Olaprixa offers a comprehensive portfolio covering wastewater treatment equipment, sludge dewatering and thickening systems, and precision chemical dosing units designed to optimize treatment performance and operational efficiency. By combining modern process engineering with automation control, the company ensures stable system operation, reduced environmental impact, and compliance with global discharge standards.
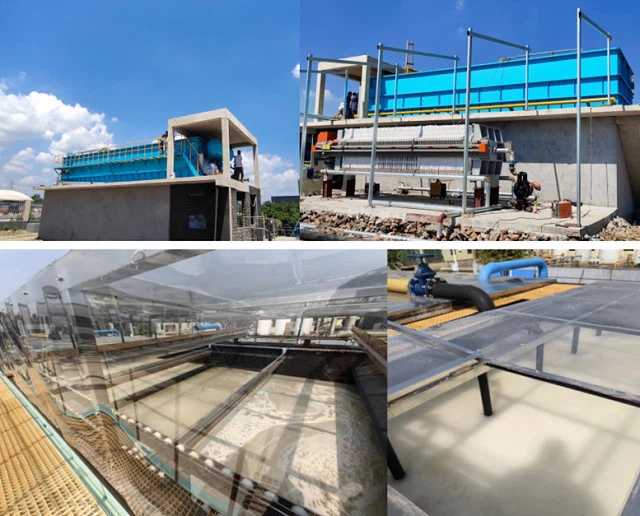
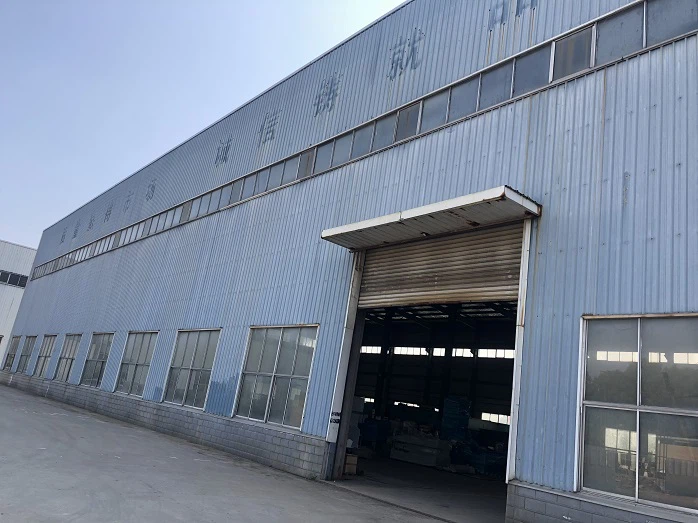
With a strong emphasis on customization, Olaprixa provides tailored water engineering solutions based on specific project requirements, from initial consultation and system design to installation guidance and after-sales technical support. Its team of experienced engineers continuously works to enhance system efficiency, reduce energy consumption, and improve resource recovery.
Committed to sustainability and innovation, Shanghai Olaprixa Industrial Co., Ltd. aims to help global clients achieve cleaner production, water reuse, and long-term environmental responsibility through smart and cost-effective treatment technologies.
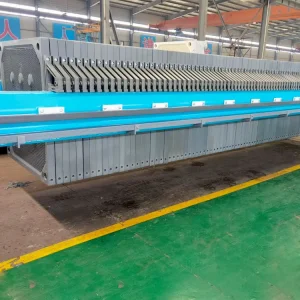
Explore our high-efficiency filtration, membrane bioreactor, and sludge processing equipment engineered for rigorous global industrial compliance.
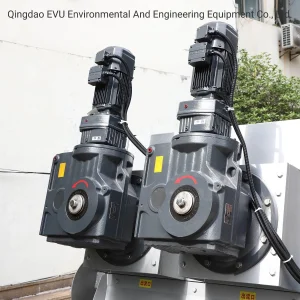
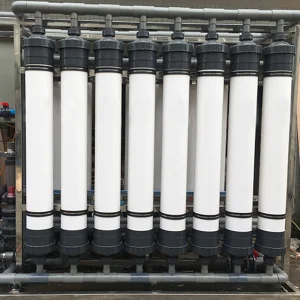
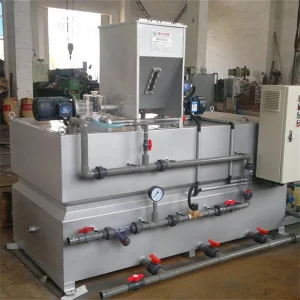
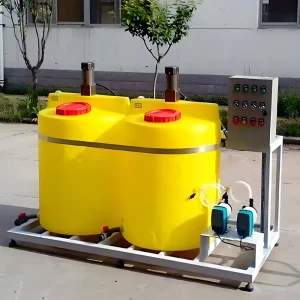
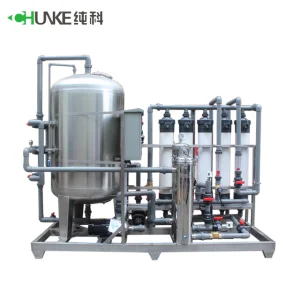
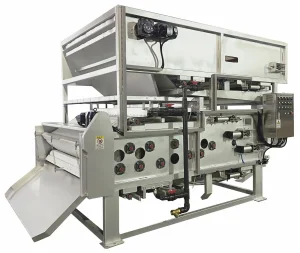
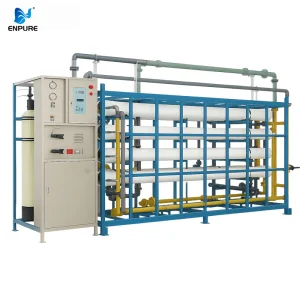
China has evolved into the world's premier manufacturing hub for advanced water treatment infrastructure, balancing massive scalability with rigorous quality engineering.
Proximity to specialized raw material suppliers, high-grade polymers, stainless steel fabrication, and smart PLC automation vendors enables rapid prototyping and cost efficiency.
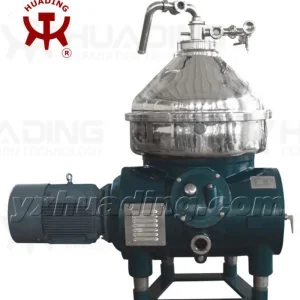
Modern Chinese factories invest heavily in membrane science, IoT-integrated dosing controllers, and energy-saving centrifuge mechanics tailored to distinct chemical loads.
Strict adherence to international benchmarks (ISO9001, CE, RoHS) ensures seamless integration into municipal and heavy industrial projects across Europe, North America, and Southeast Asia.
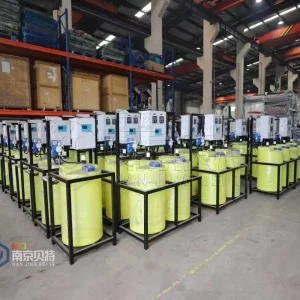
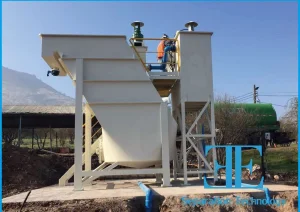
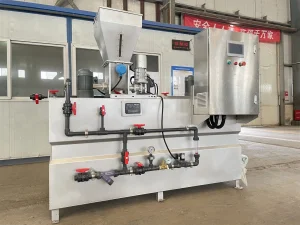
Discover specialized nanofiltration, chemical dosing, and compact clarifier units designed for maximum resource recovery and minimal footprint.
Understanding the macro shifts in sustainable water management and how modular systems deploy across varied industrial landscapes.
Driven by water scarcity, modern factories are adopting closed-loop systems combining Ultrafiltration (UF), Reverse Osmosis (RO), and Evaporation to achieve 99% water recovery.
Real-time sensor integration allows automated chemical dosing systems to react dynamically to fluctuating pollutant loads, cutting chemical waste by up to 25%.
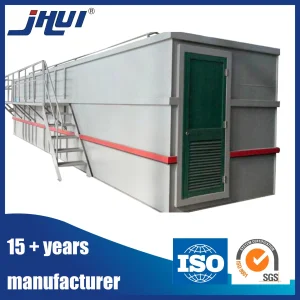
Containerized MBBR and Lamella clarifier systems enable rapid deployment in remote mining camps, municipal expansions, and disaster relief zones.
Suspended Solids Removal Efficiency
Average Energy Consumption Reduction
Global Export Markets Served
Expert answers to critical procurement, technical customization, and installation queries for industrial water treatment systems.
Selection depends on your specific influent water quality, daily flow rate, required effluent standards (e.g., local discharge limits vs. ZLD reuse), and available footprint. Our engineering team conducts full water analysis and provides customized P&ID designs.
We combine advanced engineering design, ISO-certified manufacturing in Shanghai, rigorous quality testing, and comprehensive after-sales support. Our modular equipment ensures lower capital expenditure and reliable long-term performance.
Yes. Our automated dosing units, polymer preparation systems, and filter presses feature modular PLC interfaces designed for seamless integration into existing SCADA and control networks.
Standard skid-mounted units and dosing systems typically require 4 to 6 weeks. Fully customized large-scale municipal or industrial membrane systems range from 8 to 12 weeks, depending on specification complexity.